Kerf and material use
A parallel wire web makes multiple cuts in one feed. Actual kerf depends on the wire and cutting conditions; wire diameter alone is not the measured material loss.
From blank to a qualified slicing process. Match your material, part geometry and inspection requirements to the right SOM configuration.
Discuss your partCompare models10 моделей SOM · 6 групп применения · Бесплатная резка образцов
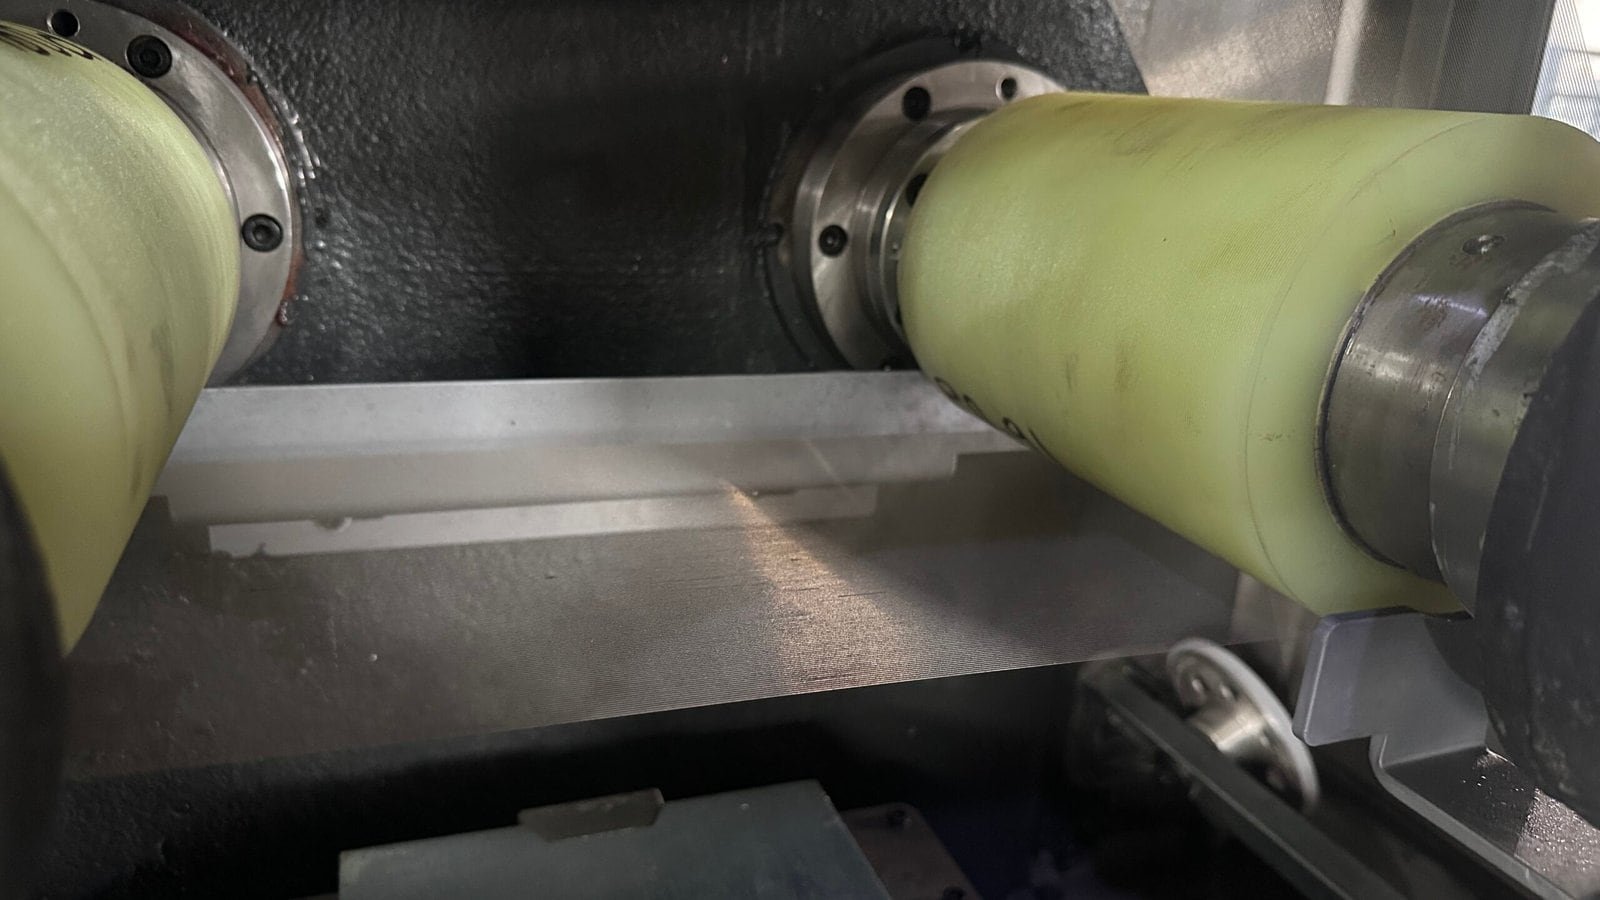
A parallel wire web makes multiple cuts in one feed. Actual kerf depends on the wire and cutting conditions; wire diameter alone is not the measured material loss.
Wire pitch and actual kerf determine the as-cut slice thickness. Allow separately for grinding or polishing before specifying the finished dimension.
Review support, fixture clearance and release of the slices. Assess edge chipping and surface condition on your material before fixing the production settings.
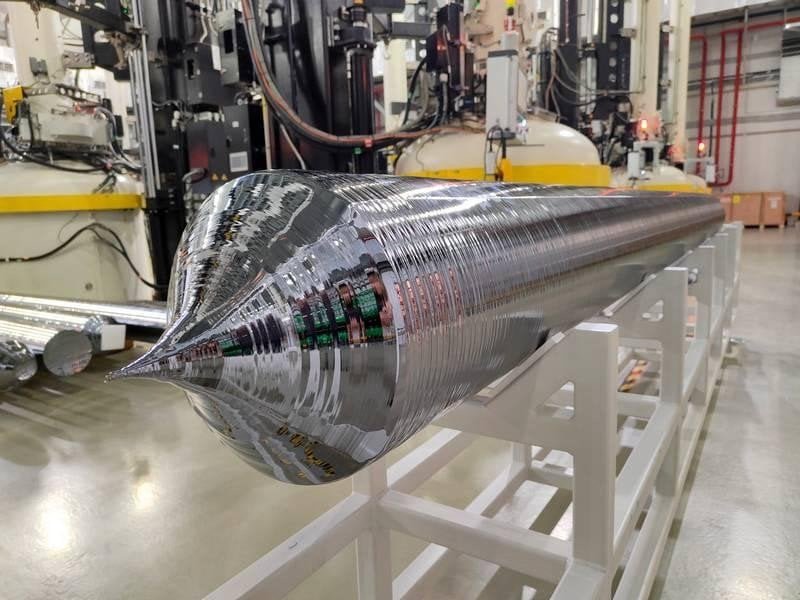
Crop and prepare the ingot to suit the machine envelope before loading.
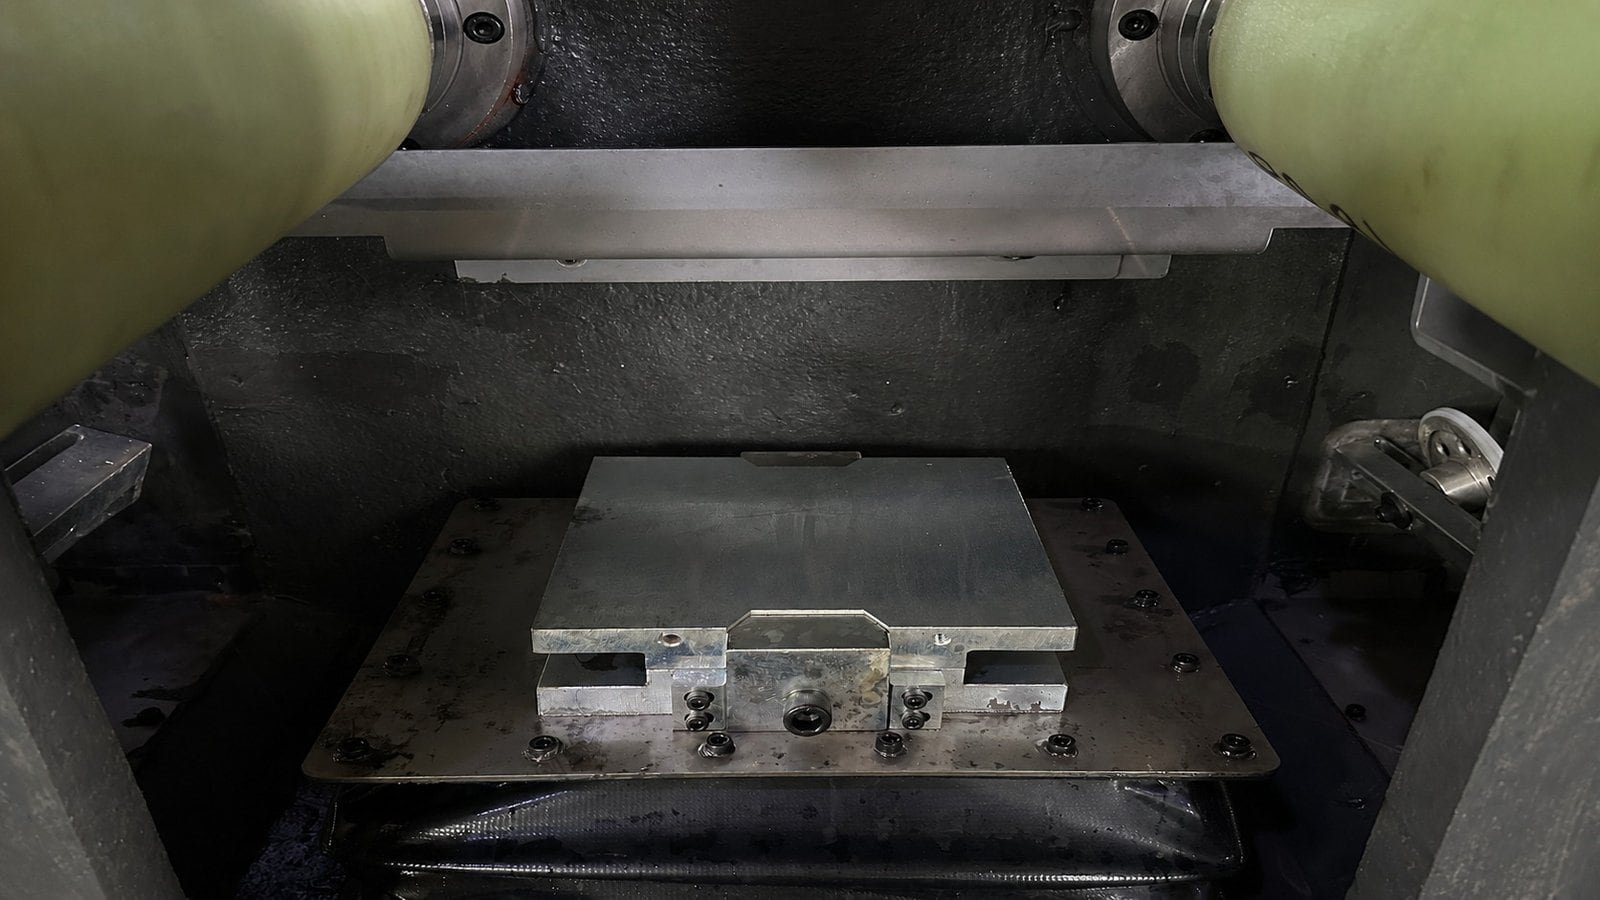
SOM200 fixture before loading. Review support and clearance for the prepared blank.
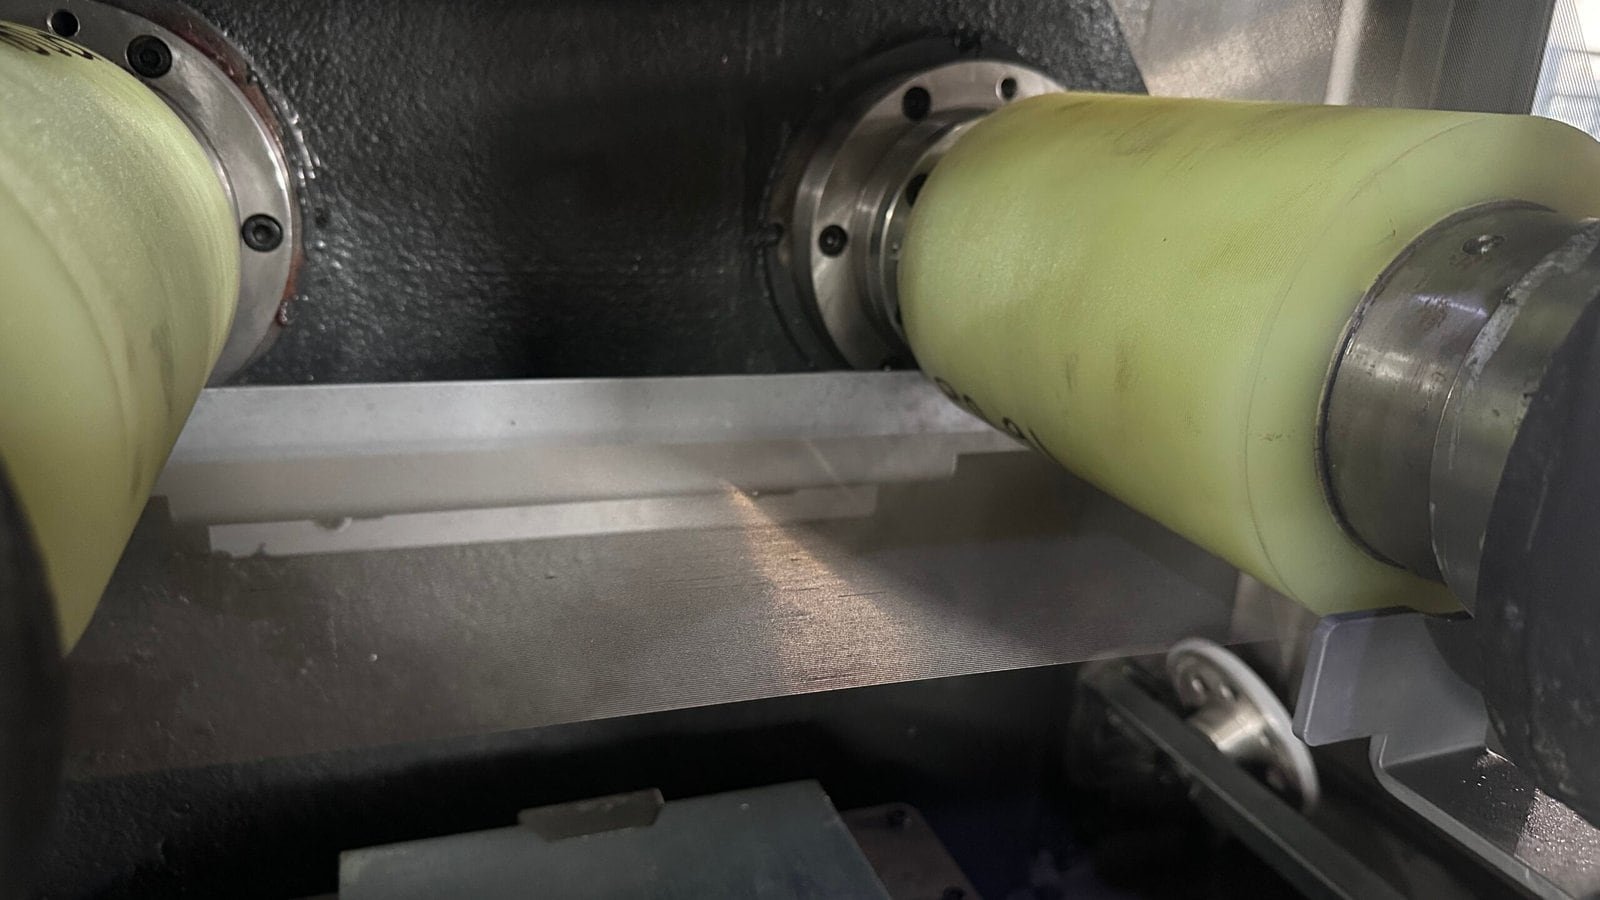
Parallel wire web and guide rollers. Set the cutting conditions for the material and slice requirement.
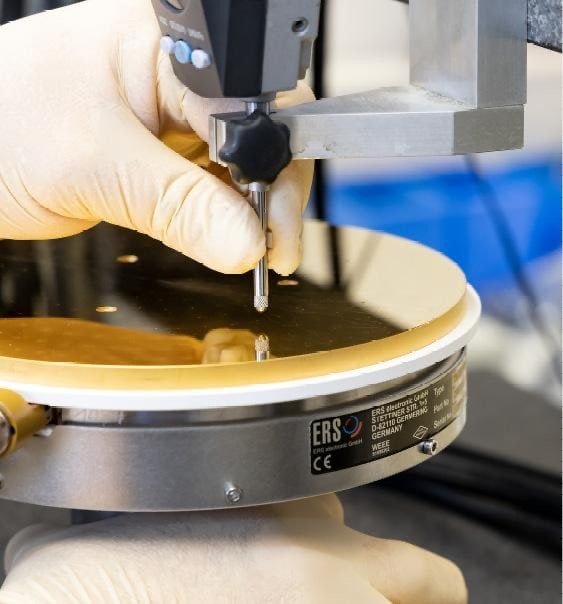
Contact-probe inspection. Agree the measurement method and acceptance criteria for your part.
Images illustrate the individual stages; they do not document a single workpiece or one continuous production run.
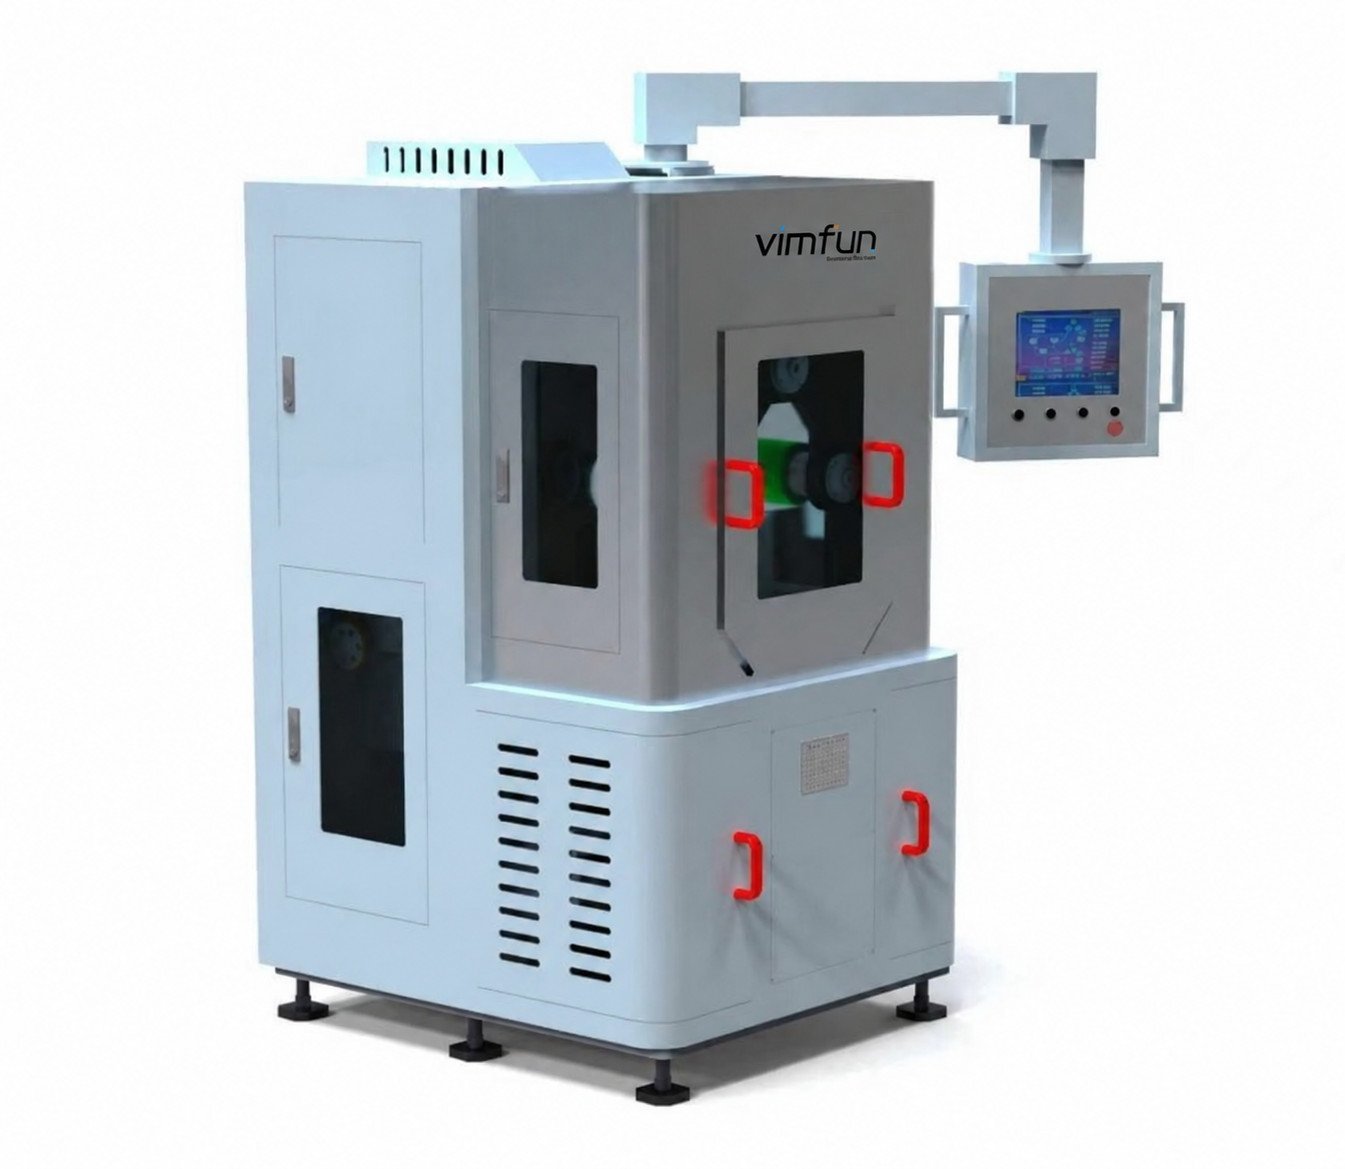
Start with the workpiece and cutting route. Then compare the listed envelope and slice range with your fixture and finishing requirements.
Компактное решение для малых партий, частой смены материалов и разработки процессов. Начните с этого, если полномасштабная производственная машина превысит требования к заготовке и партии.
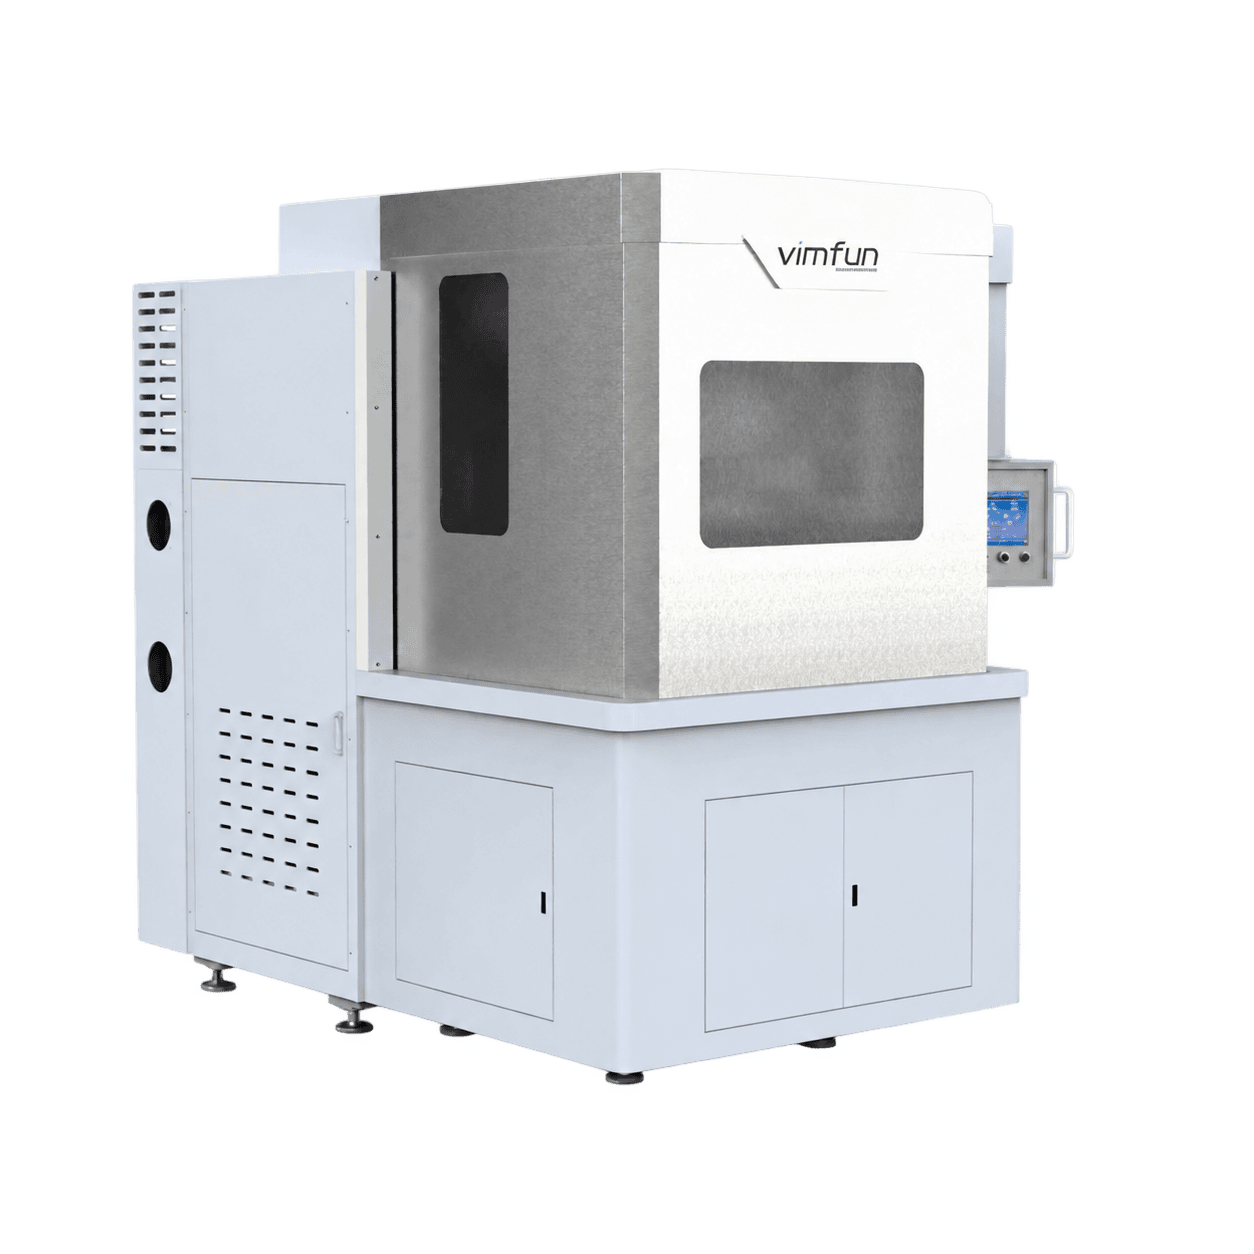
Отдавайте приоритет этой модели, когда поперечное сечение заготовки является ограничением. Ее двухплатформенная компоновка отличается от простого удлинения узкой заготовки. Проверьте двухплатформенную компоновку с вашей оснасткой.
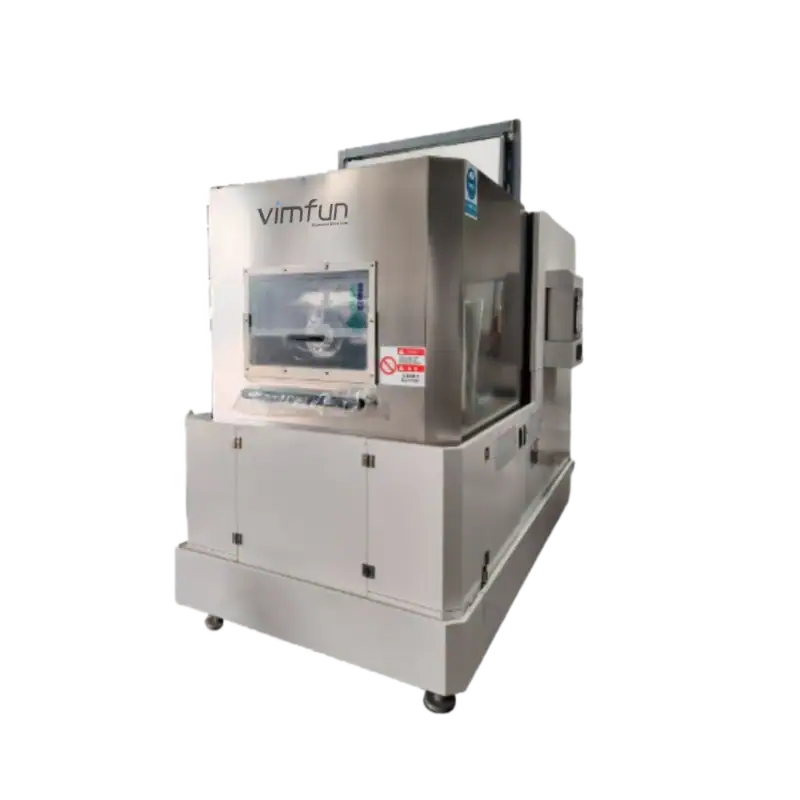
Для квадратной обработки кремниевых слитков и твердых, хрупких заготовок с более узким поперечным сечением. Подтвердите предлагаемый диапазон срезов по вашему чертежу перед выбором шага проволочной сетки.
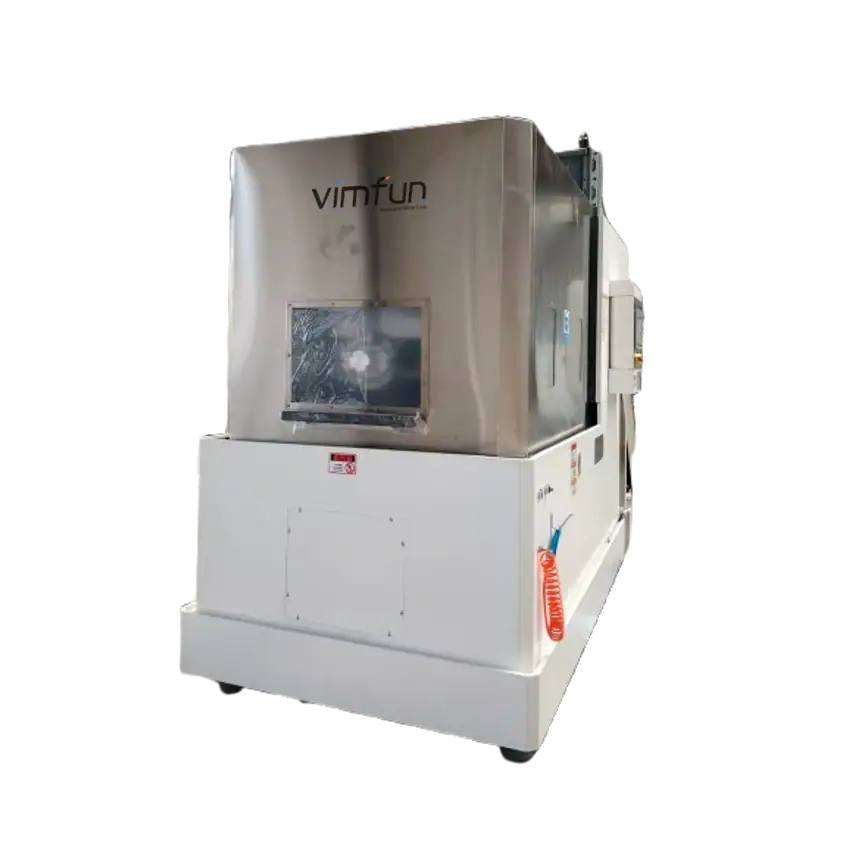
Рассмотрите эту модель для длинных заготовок серийного производства. Проверьте ширину и высоту, а также длину: более длинная машина не принимает автоматически большее поперечное сечение, обрабатываемое SOM400.
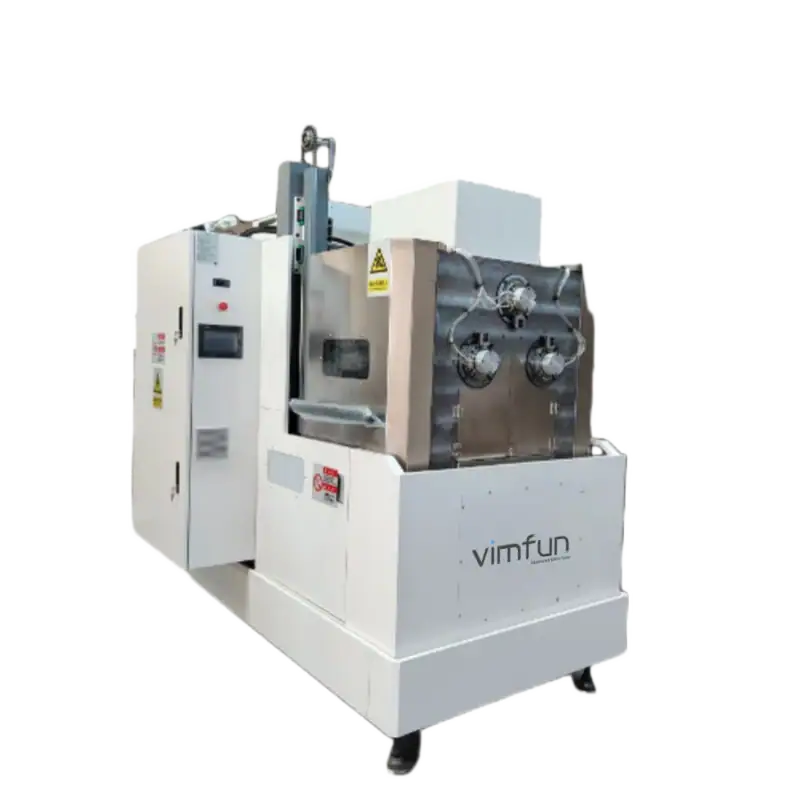
Для серийного производства тонких срезов из твердых материалов. Сравните требуемый диапазон толщин с SOMIS-400 и оцените состояние поверхности, поддержку оснастки и полное время цикла на фактическом материале.
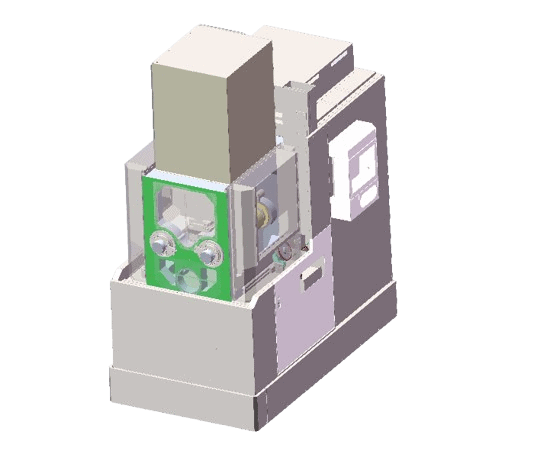
Опция перевернутой резки для более коротких заготовок и тонких срезов. Проверьте компоновку крепления и требуемый припуск на обработку вместе; указанный диапазон срезов не является допуском на готовую пластину.
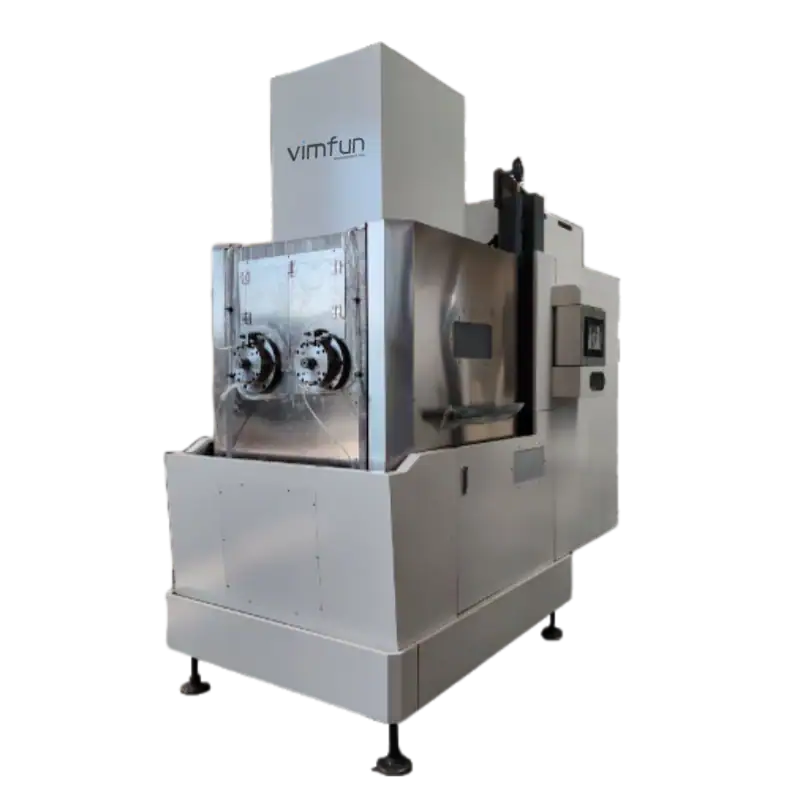
Для более длинных заготовок, чем SOMI-430, в пределах той же указанной ширины и высоты. Указанная максимальная скорость возвратно-поступательного движения проволоки составляет 2200 м/мин; рабочая скорость должна быть выбрана в зависимости от материала и результата испытания.
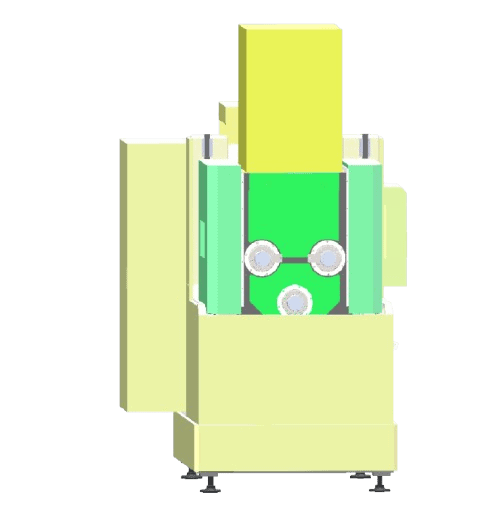
Планируемый маршрут для карбида кремния и оксида алюминия, с сапфиром также в пределах области применения. Сравните этот более широкий диапазон толщин с SOMS3-430, когда рассматриваются как поворотный механизм, так и тонкие срезы.
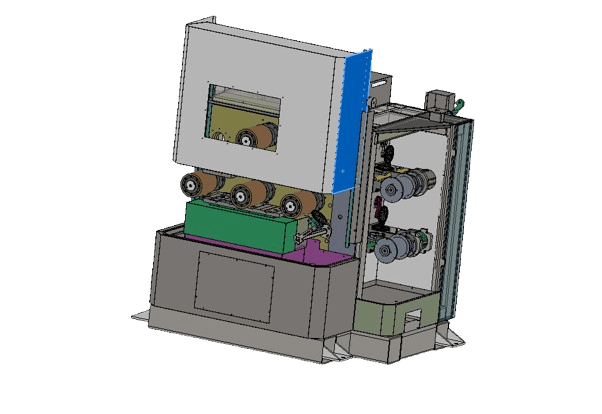
Для небольших магнитных блоков и производства прямых срезов. Определите толщину после резки отдельно от окончательной толщины после шлифовки и включите пространство для удержания и поддержку края при рассмотрении загрузки.
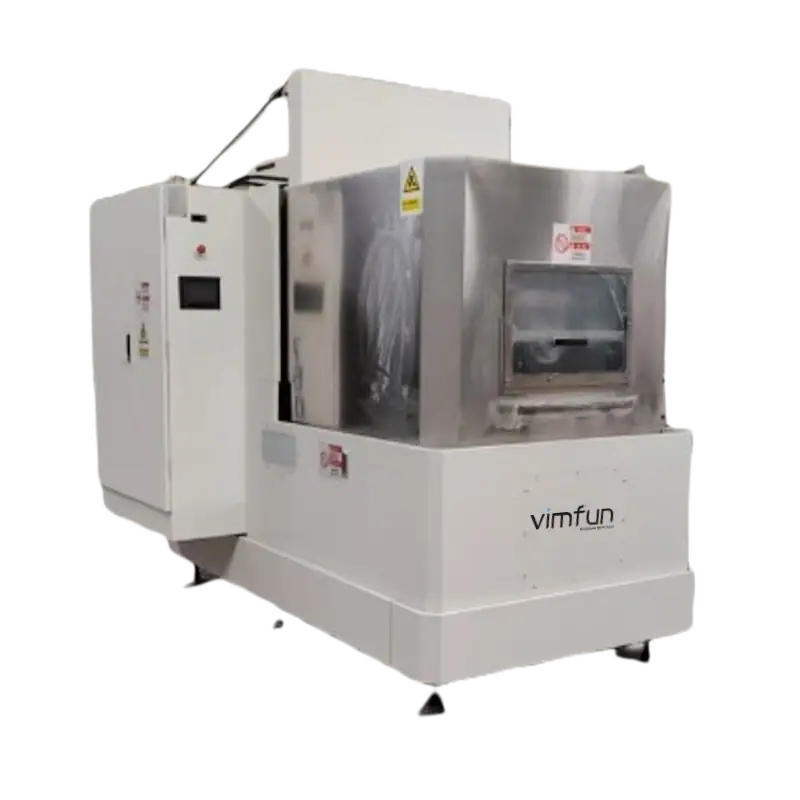
Для более длинных магнитных заготовок и комбинации прямых срезов и дуговых сегментов. Отправьте внутренний радиус, внешний радиус и толщину изогнутых деталей, чтобы можно было оценить маршрут резки и последующей шлифовки.
Dimensions marked × 2 refer to two workstations. Listed slice ranges are not finished-part tolerances. Product images show equipment configurations; confirm the ordered arrangement.
Explore the material guides to narrow the cutting route, machine configuration and sample requirements.
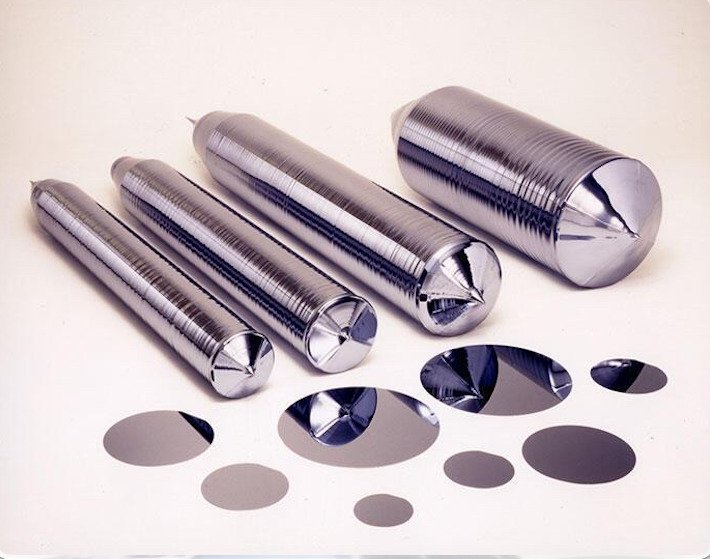
Thin slices, finishing stock and thickness inspection.
Explore application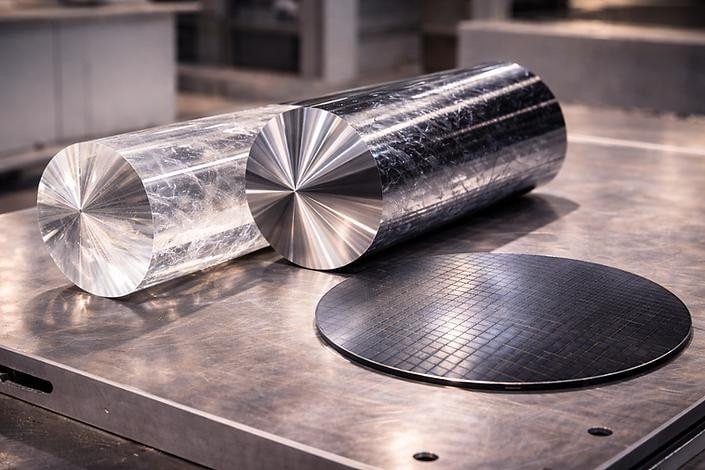
Review the cutting route and surface condition on a trial.
Explore application
Define crystal orientation, cut geometry and edge criteria.
Explore application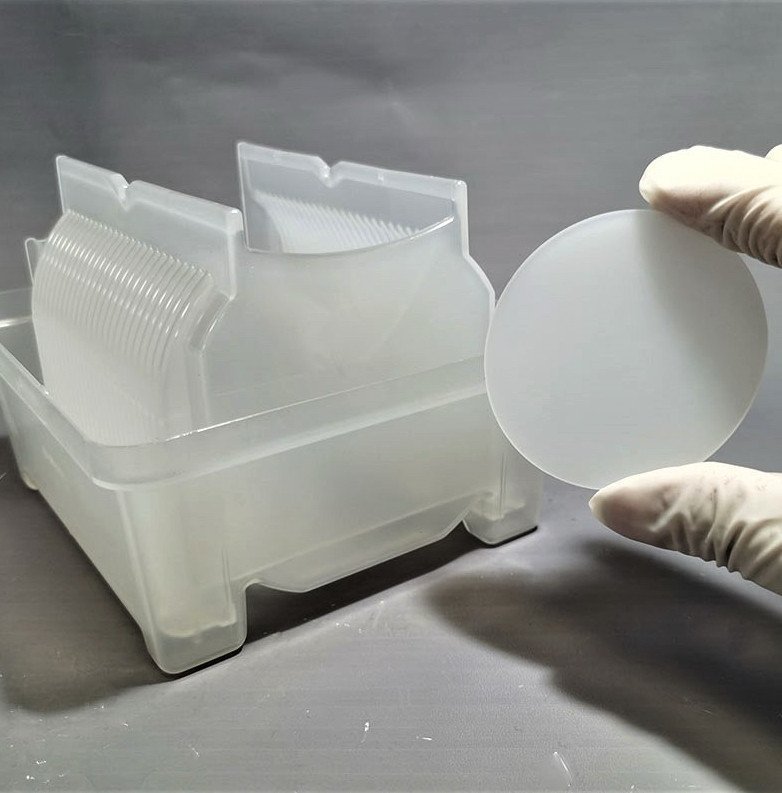
Review wafer support, slice thickness and finishing allowance.
Explore application
Define magnetized state, slice geometry and grinding allowance.
Explore applicationNeed individual sections rather than parallel batches? Compare wire sawing and sectioning methods.