Kerf and material use
A parallel wire web makes multiple cuts in one feed. Actual kerf depends on the wire and cutting conditions; wire diameter alone is not the measured material loss.
From blank to a qualified slicing process. Match your material, part geometry and inspection requirements to the right SOM configuration.
Discuss your partCompare models10 SOMモデル · 6つのアプリケーショングループ · 無料サンプルカット
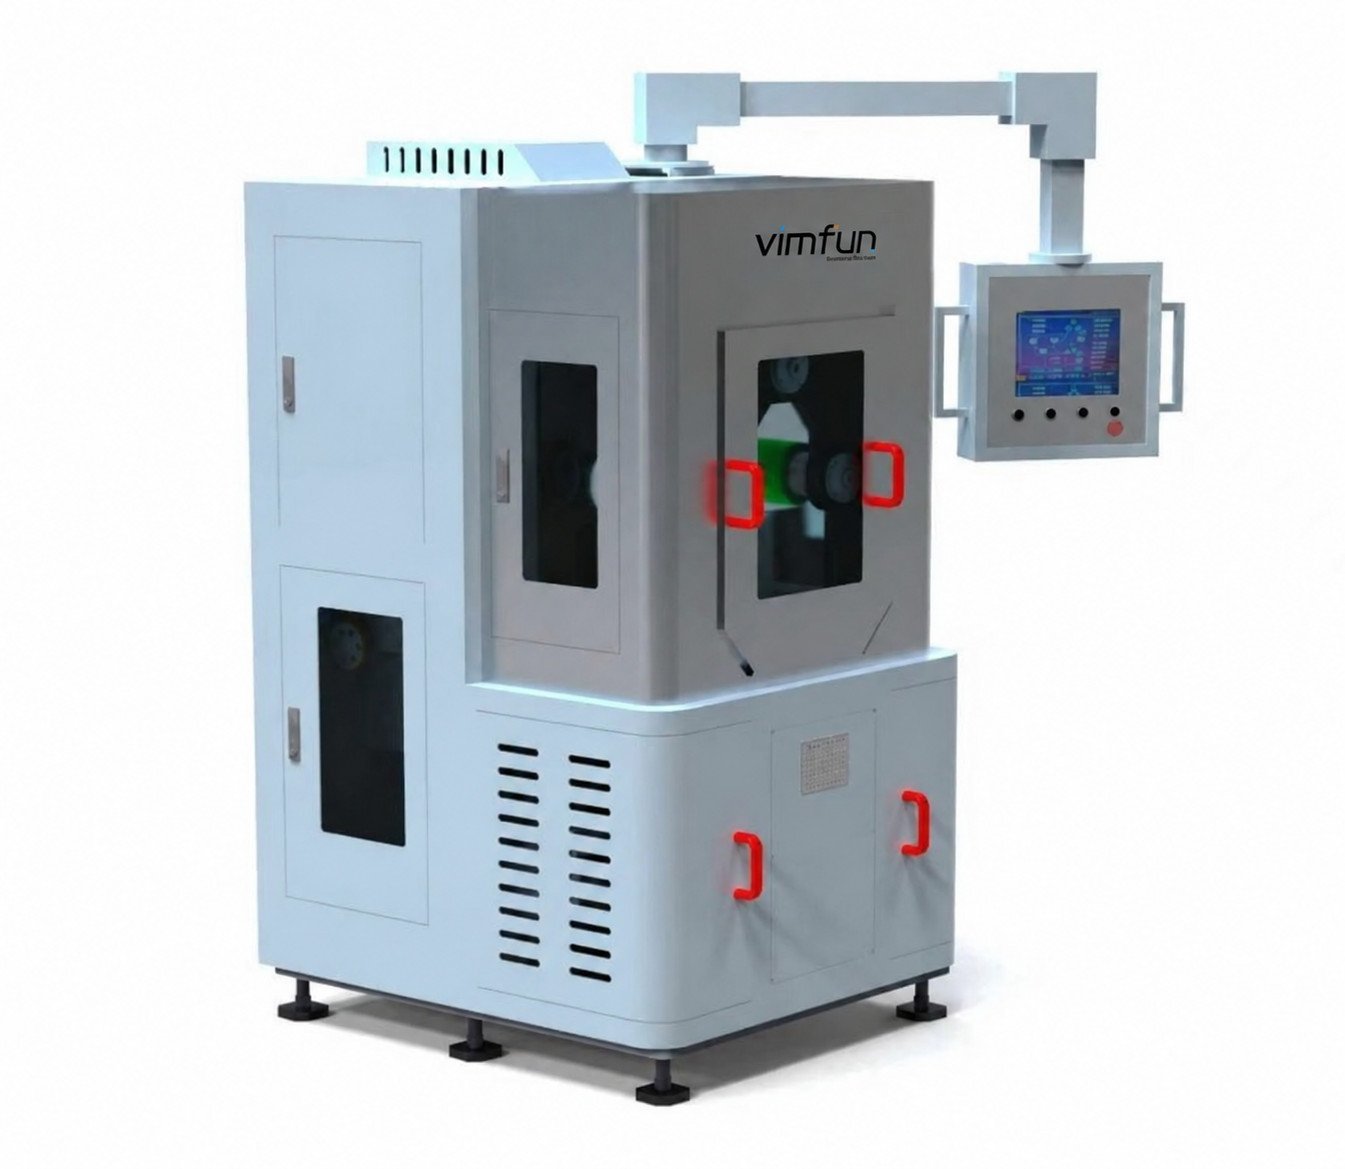
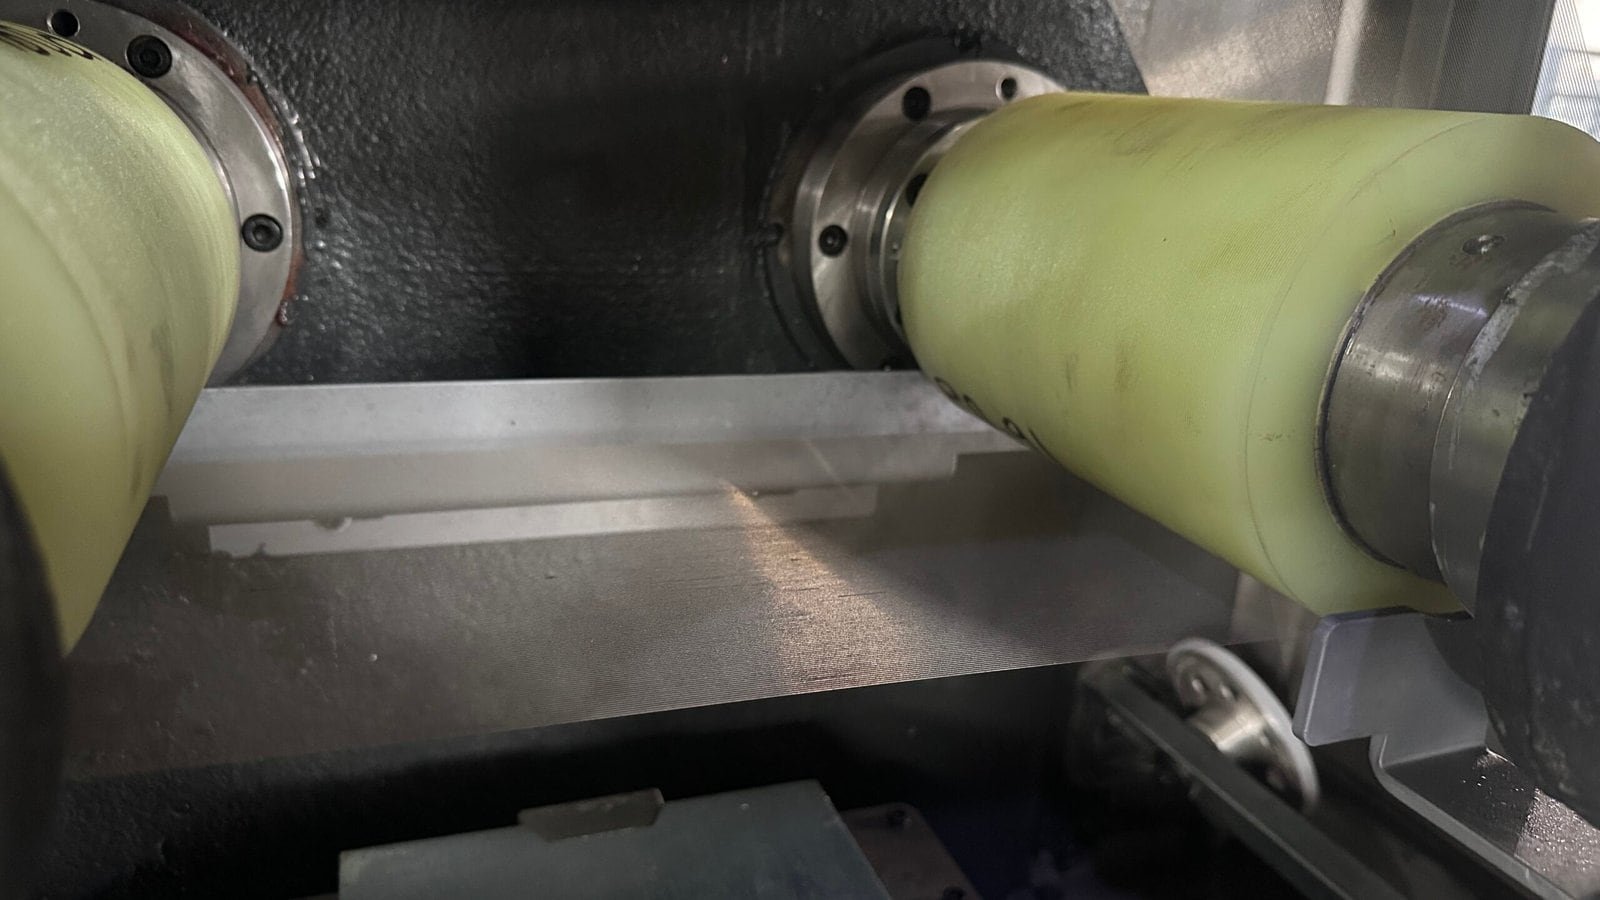
A parallel wire web makes multiple cuts in one feed. Actual kerf depends on the wire and cutting conditions; wire diameter alone is not the measured material loss.
Wire pitch and actual kerf determine the as-cut slice thickness. Allow separately for grinding or polishing before specifying the finished dimension.
Review support, fixture clearance and release of the slices. Assess edge chipping and surface condition on your material before fixing the production settings.
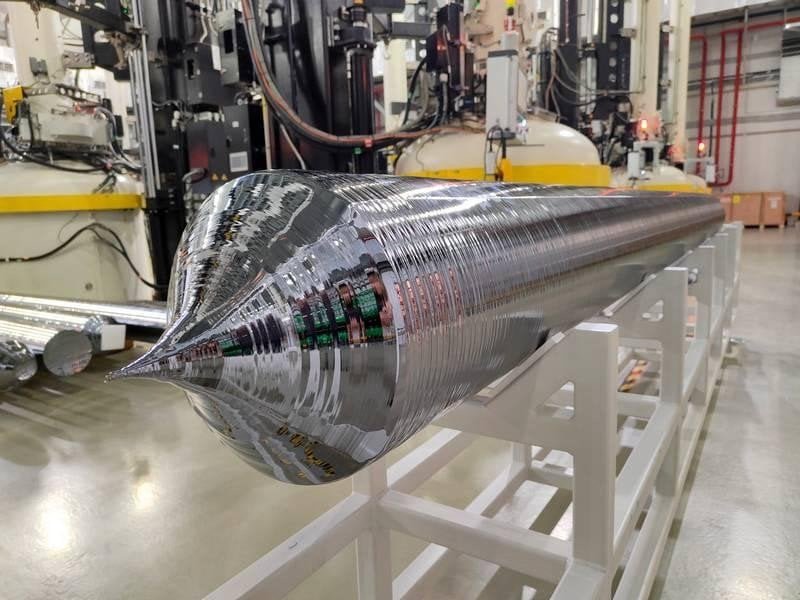
Crop and prepare the ingot to suit the machine envelope before loading.
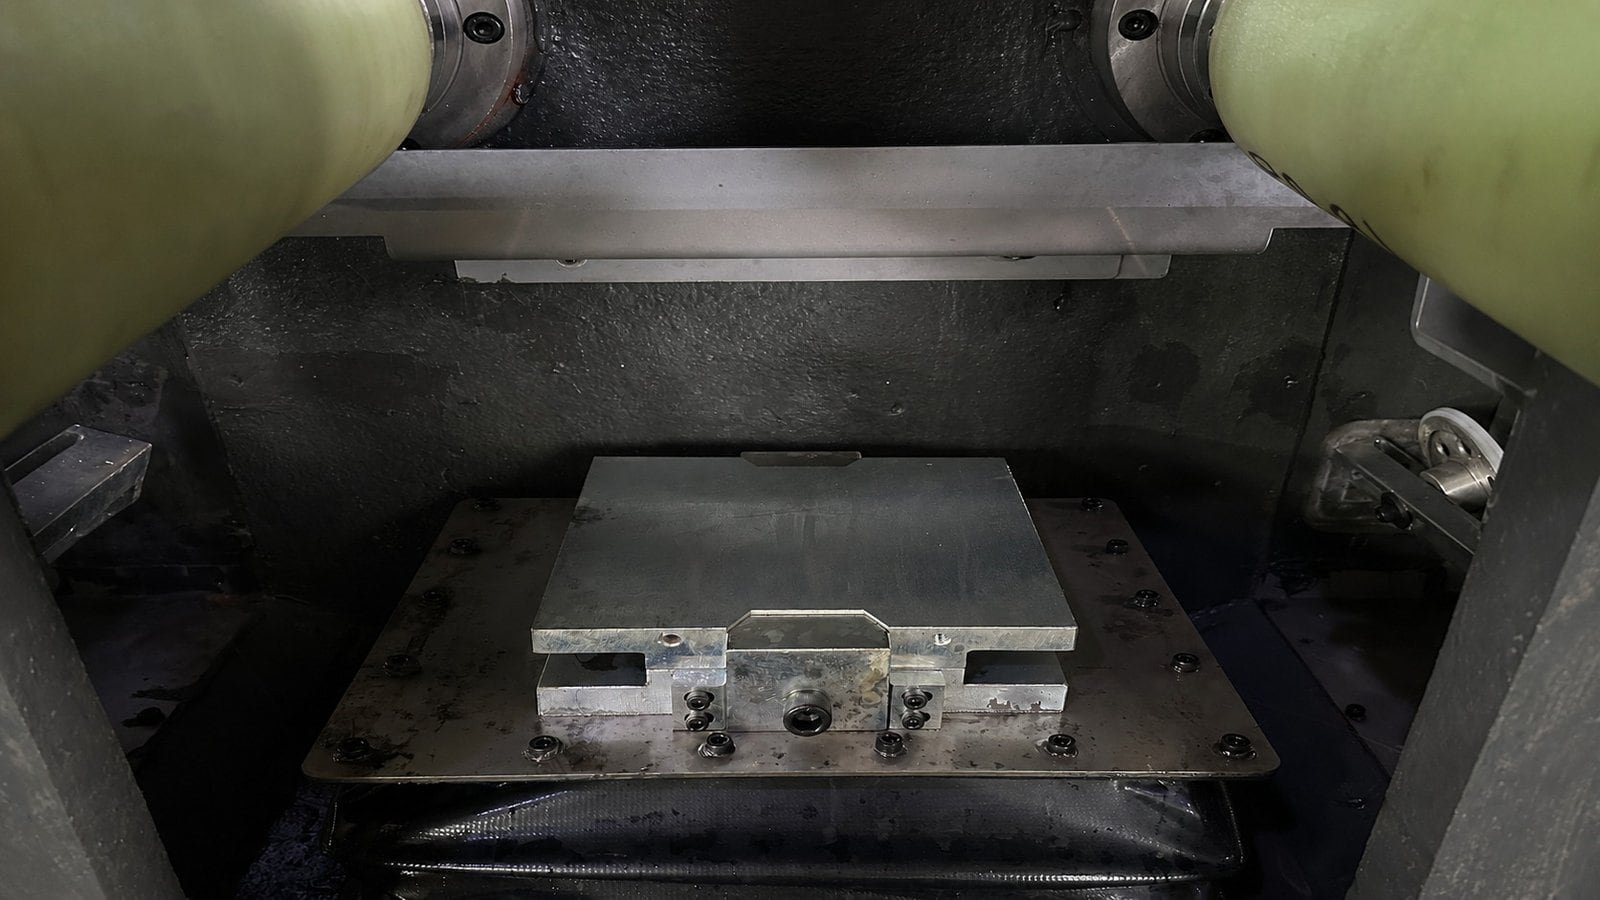
SOM200 fixture before loading. Review support and clearance for the prepared blank.
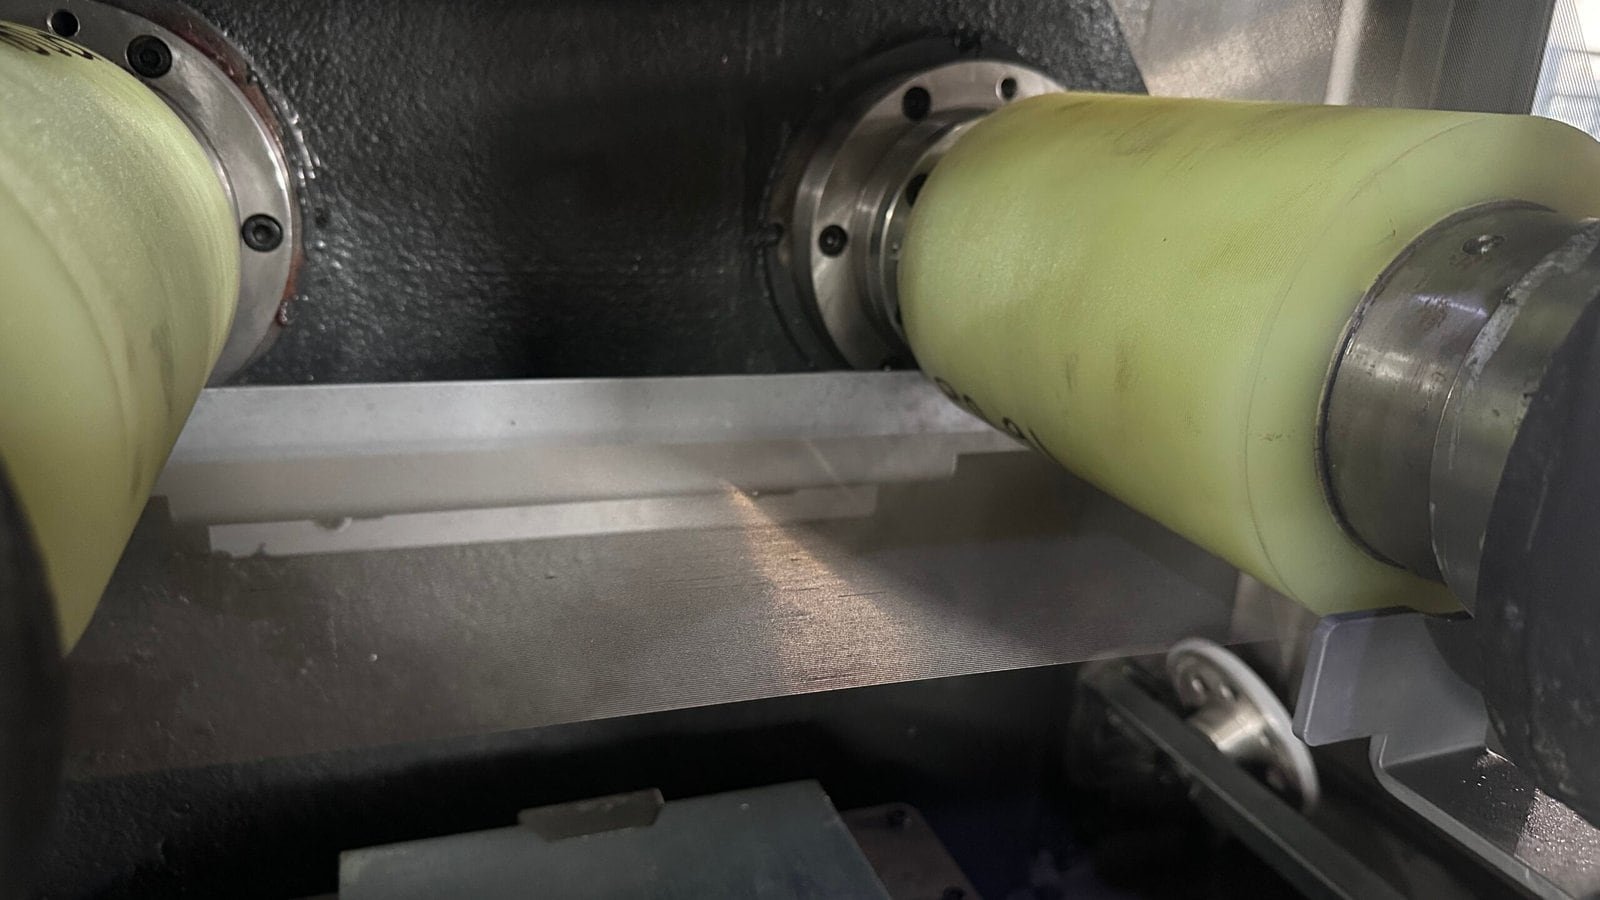
Parallel wire web and guide rollers. Set the cutting conditions for the material and slice requirement.
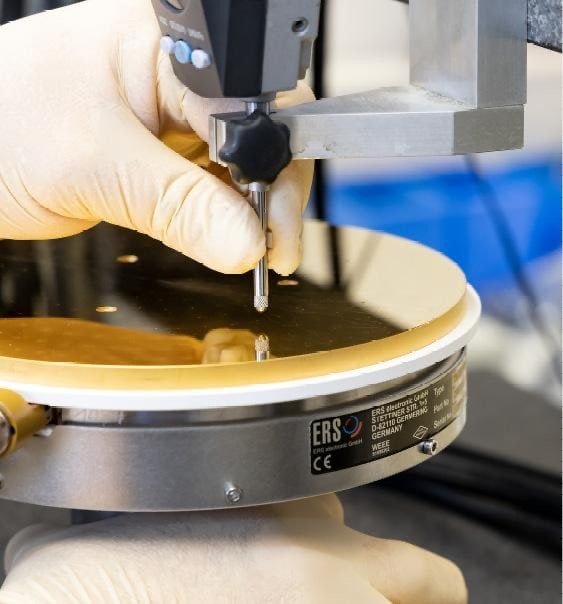
Contact-probe inspection. Agree the measurement method and acceptance criteria for your part.
Images illustrate the individual stages; they do not document a single workpiece or one continuous production run.
Start with the workpiece and cutting route. Then compare the listed envelope and slice range with your fixture and finishing requirements.
小ロット、頻繁な材料変更、およびプロセス開発向けのコンパクトなオプション。フル生産機がワークピースおよびロットの要件を超える場合は、ここから開始してください。.
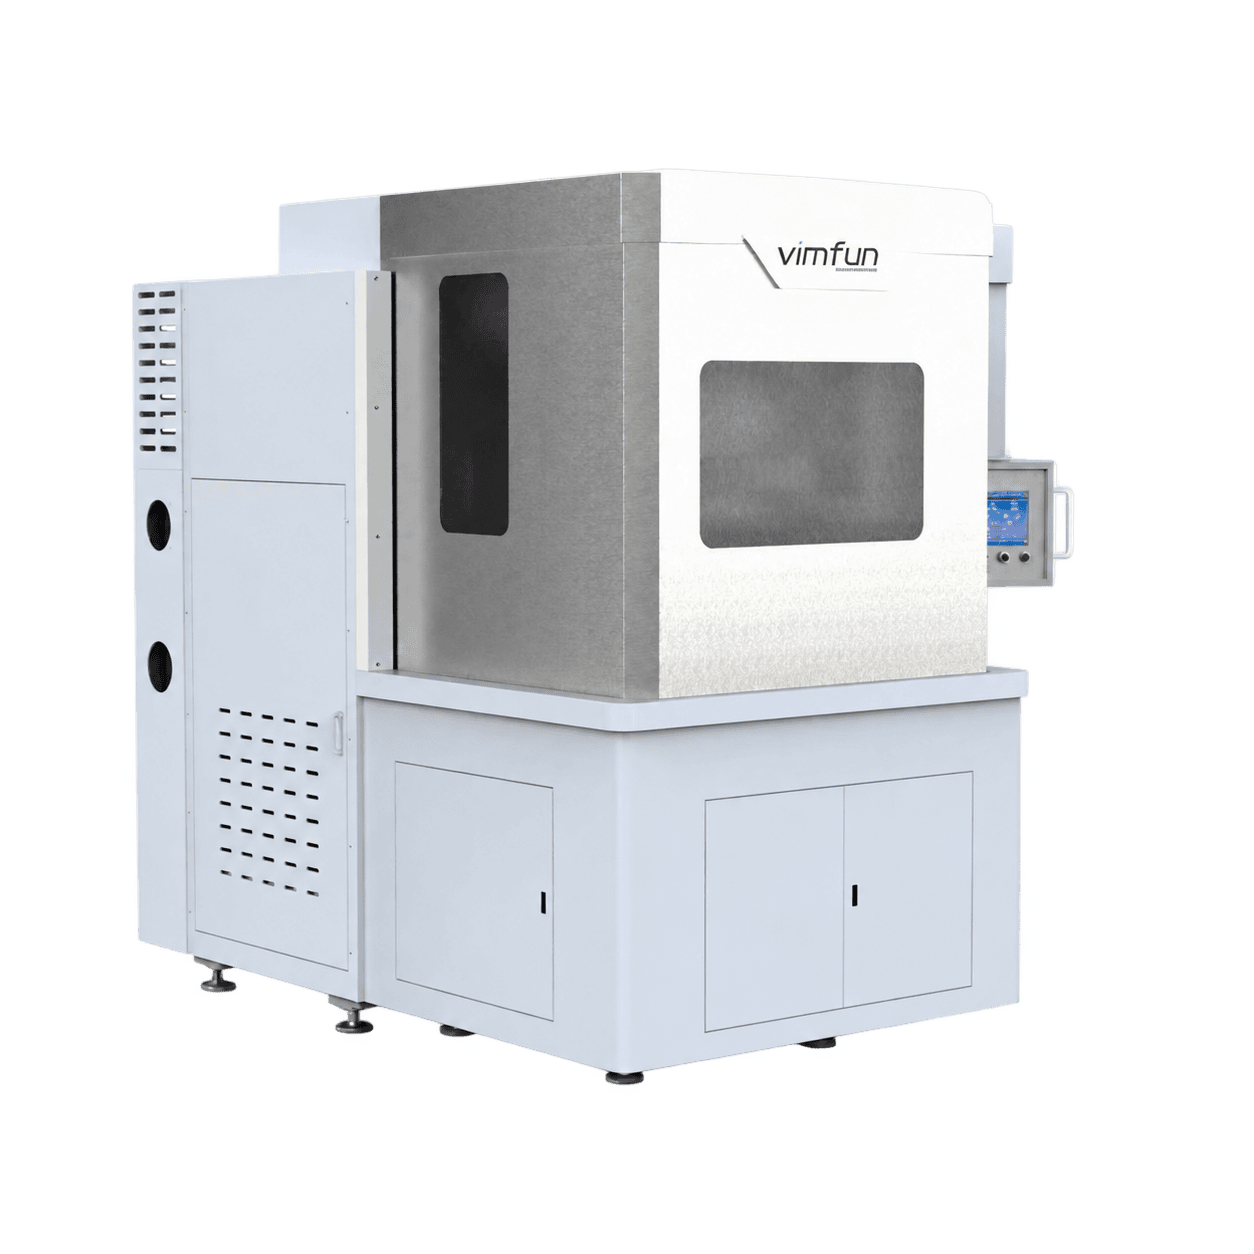
ワークピースの断面が制約となる場合は、このモデルを優先してください。そのデュアルワークプレート配置は、単に細いビレットの長さを延長するのとは異なります。2枚プレートのレイアウトを治具とともに確認してください。.
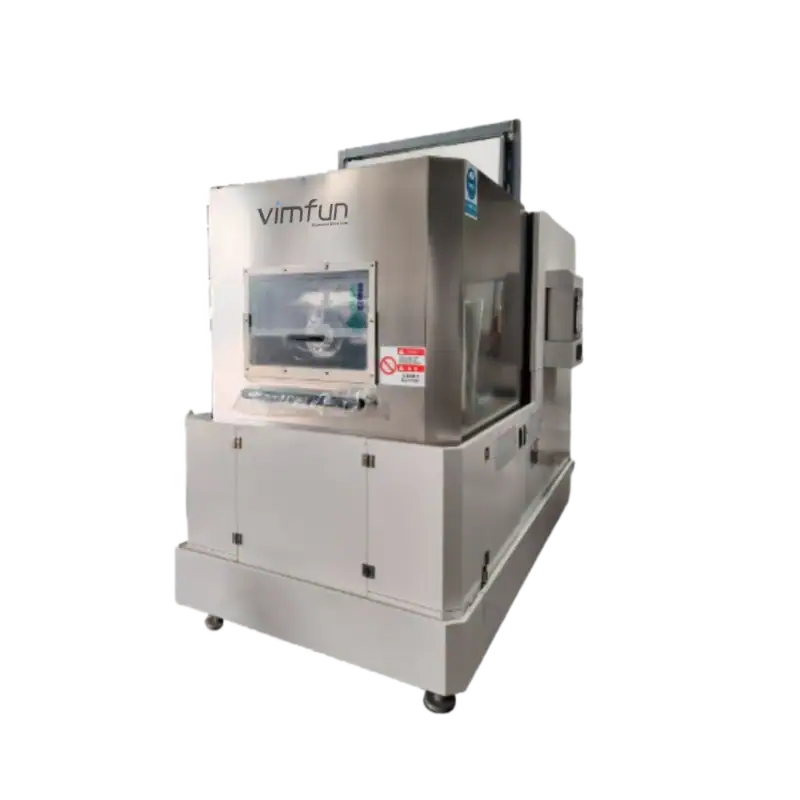
シリコンインゴットのスクエア加工および硬質脆性ワークピースの、より狭い断面向け。ワイヤーピッチを選択する前に、提案されたスライス範囲を図面と照合して確認してください。.
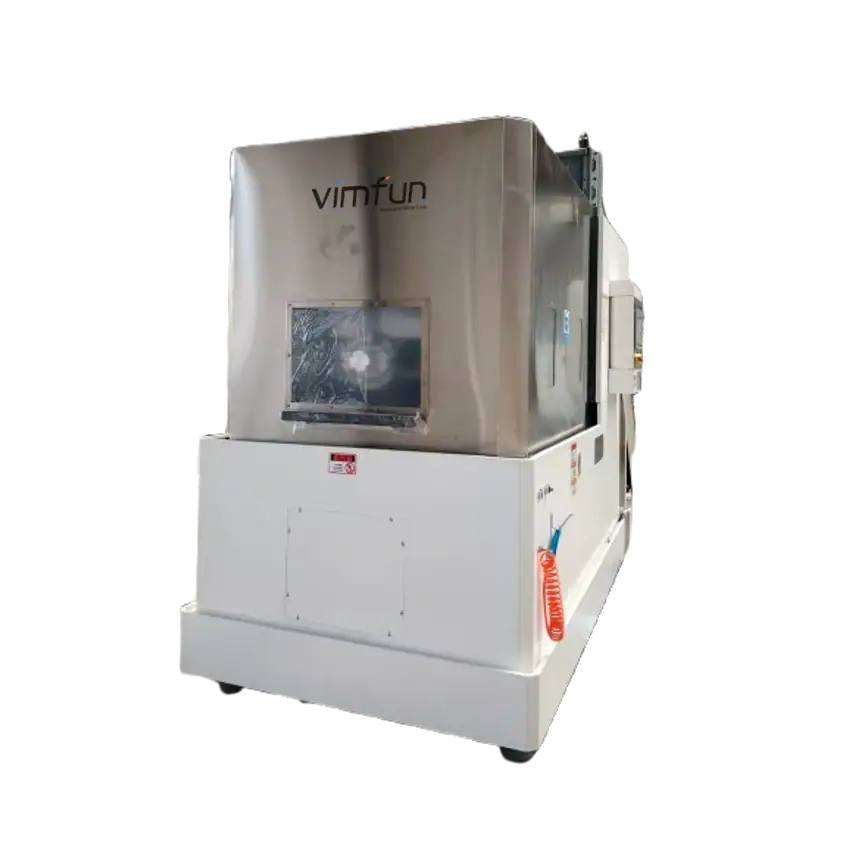
長尺の繰り返し生産ワークピース向けにこのモデルを検討してください。幅と高さだけでなく、長さも確認してください。より長い機械であっても、SOM400が処理するより大きな断面を自動的に受け入れられるわけではありません。.
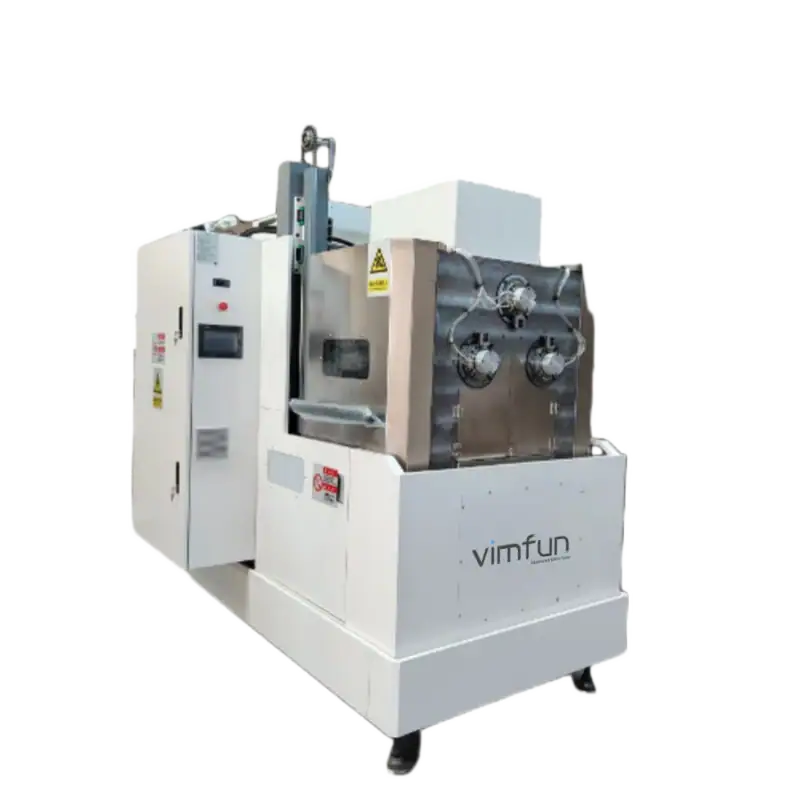
薄い硬質材料スライスの繰り返し生産向け。必要とされる厚み範囲をSOMIS-400と比較し、実際の材料で表面状態、治具サポート、および完全なサイクルタイムを評価してください。.
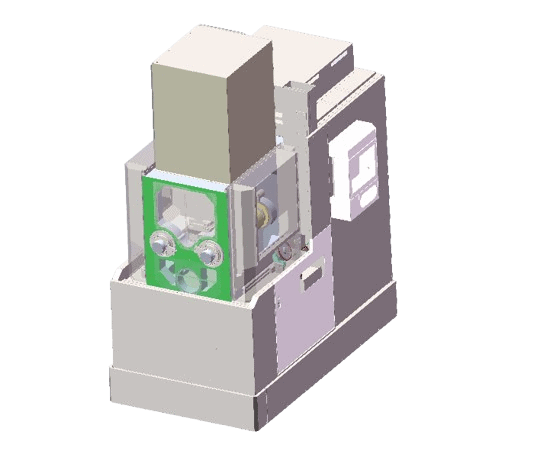
短いワークピースと薄いスライス向けの逆送りカットオプション。取り付け配置と必要な仕上げしろを一緒に確認してください。記載のスライス範囲は、仕上げ済みウェーハの公差ではありません。.
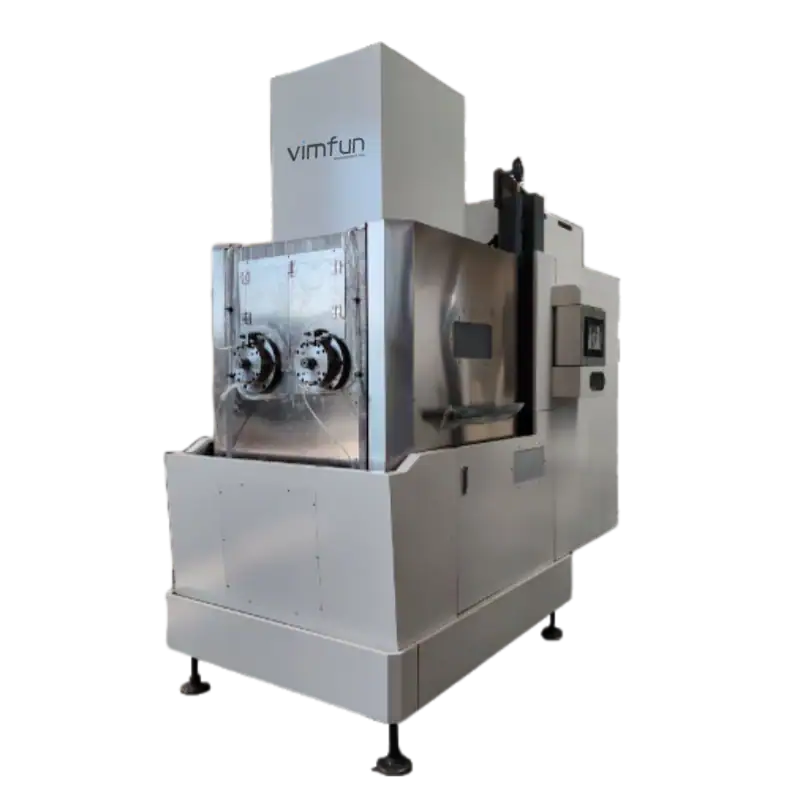
同じ記載幅と高さ内で、SOMI-430よりも長いワークピース向け。指定された最大往復ワイヤー速度は2,200 m/minです。作業速度は、材料とトライアル結果に合わせて選択する必要があります。.
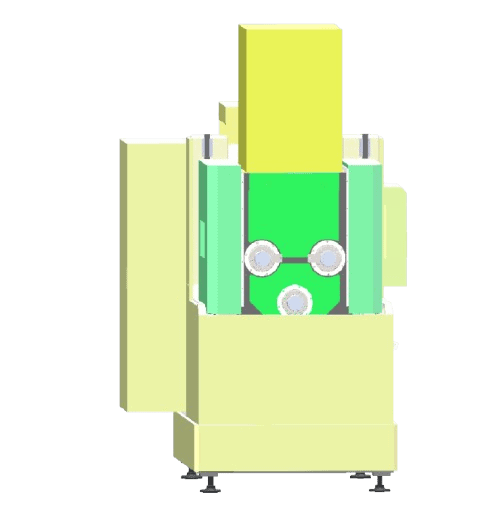
炭化ケイ素およびアルミナ向けの計画ルート。サファイアもアプリケーション範囲内です。スイング機構と薄いスライスの両方が検討されている場合は、このより広い厚み範囲をSOMS3-430と比較してください。.
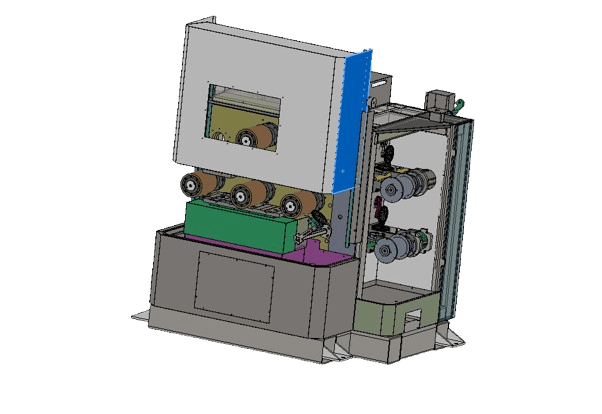
小型マグネットブロックおよびストレートスライス生産向け。カット時の厚みと最終研磨厚みを別々に定義し、保持スペースとエッジサポートを積載レビューに含めてください。.
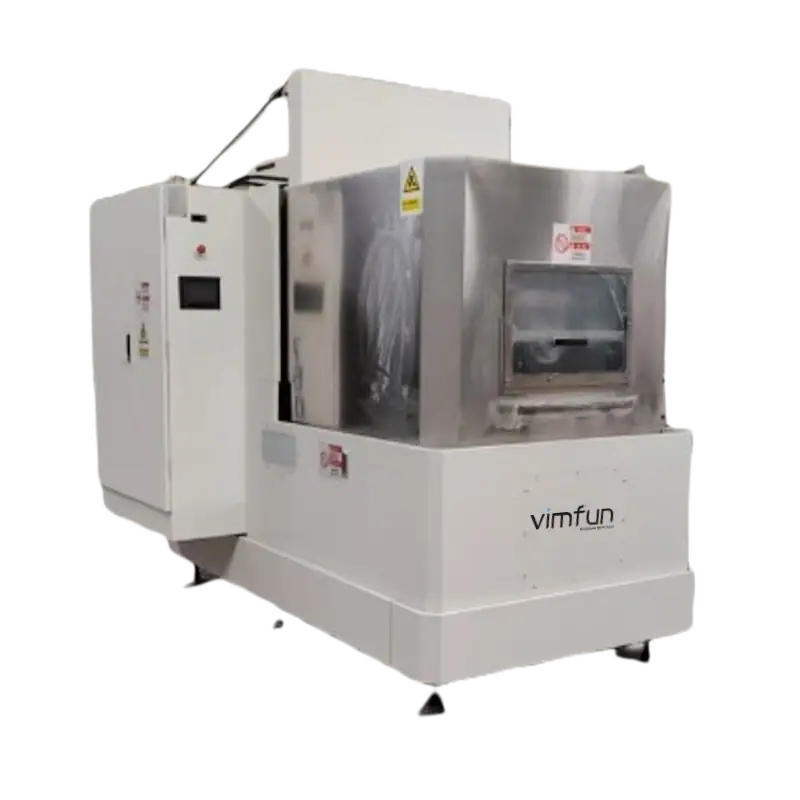
長尺マグネットワークピースおよびストレートスライスとアークセグメントの混合向け。曲げ部品の内半径、外半径、および厚みを送信して、カットおよび後続の研磨ルートを評価できるようにしてください。.
Dimensions marked × 2 refer to two workstations. Listed slice ranges are not finished-part tolerances. Product images show equipment configurations; confirm the ordered arrangement.
Explore the material guides to narrow the cutting route, machine configuration and sample requirements.
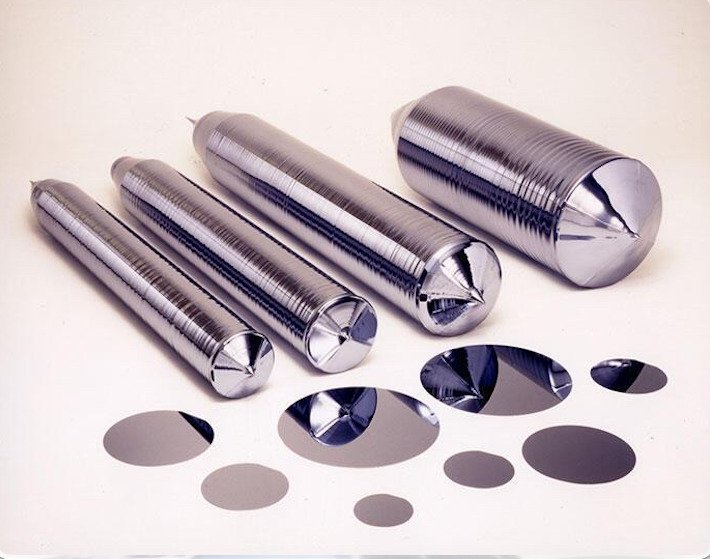
Thin slices, finishing stock and thickness inspection.
Explore application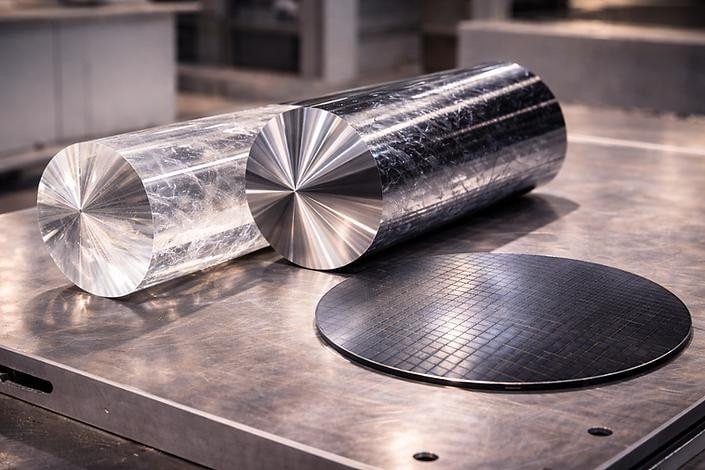
Review the cutting route and surface condition on a trial.
Explore application
Define crystal orientation, cut geometry and edge criteria.
Explore application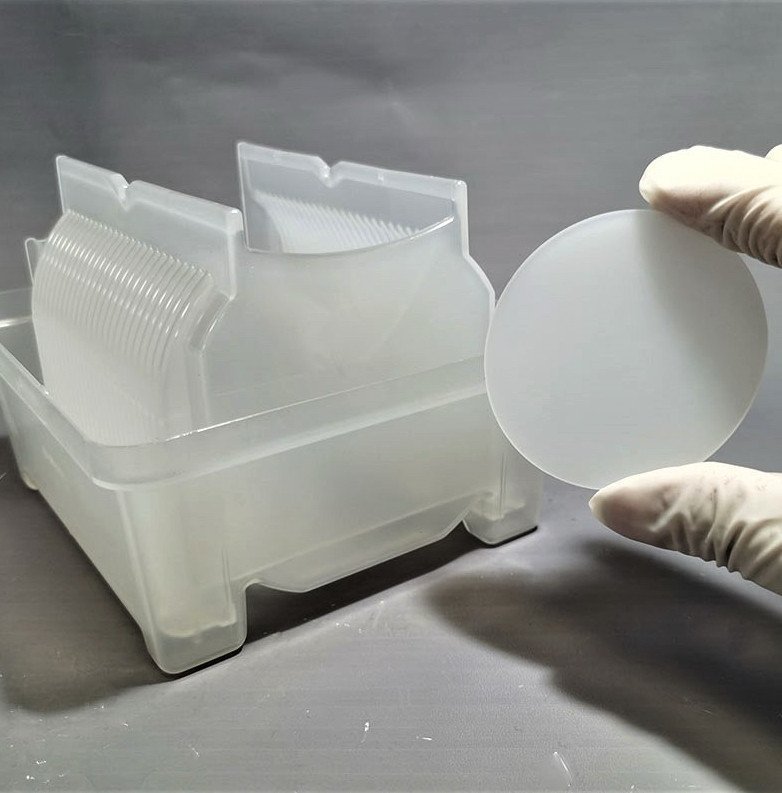
Review wafer support, slice thickness and finishing allowance.
Explore application
Define magnetized state, slice geometry and grinding allowance.
Explore applicationNeed individual sections rather than parallel batches? Compare wire sawing and sectioning methods.